Industrial Reverse Osmosis (RO) Pure Water Systems
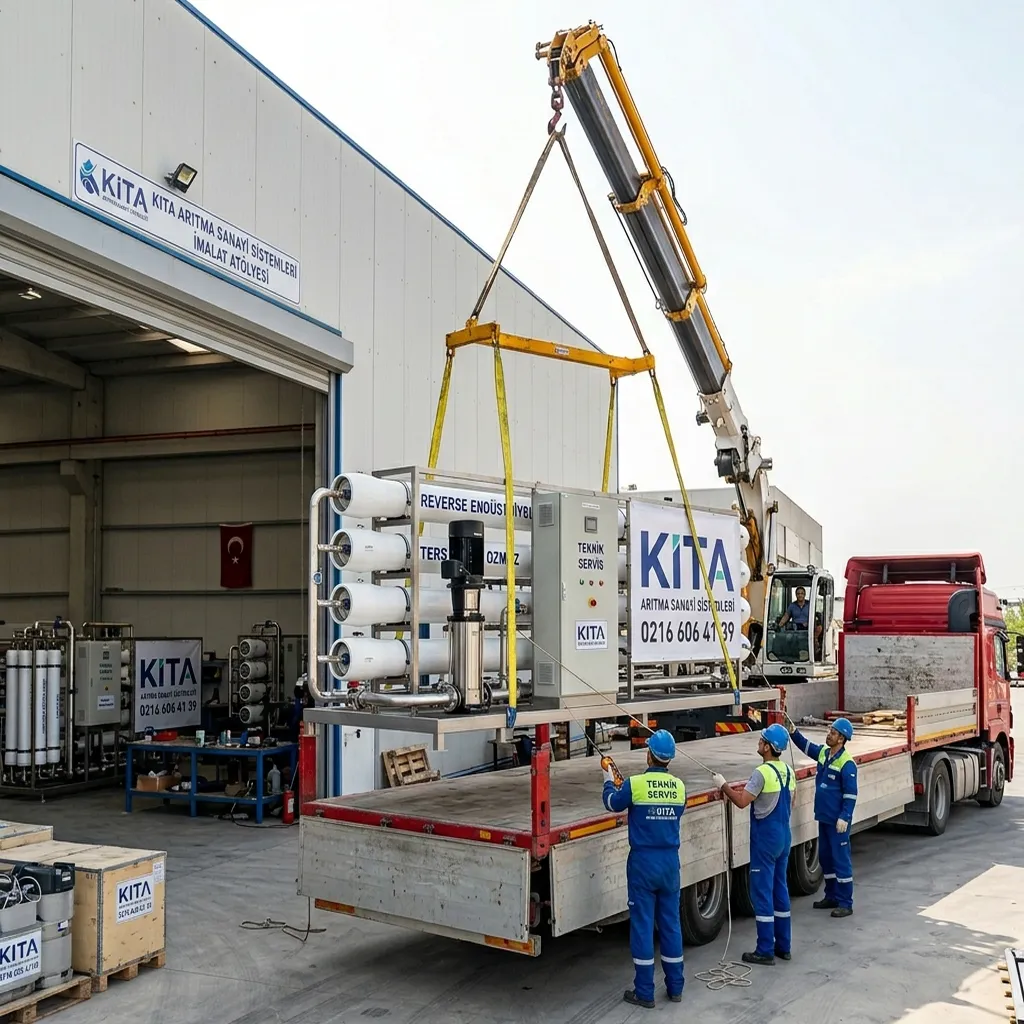
PLC-controlled industrial RO with 4040/8040 membranes removing 95–99.5% of dissolved salts.
- 0.25 – 100+ m³/h
- Reverse osmosis, TFC polyamide…
Industry solution
Consistent, analysed process and drinking water for product quality, shelf life and food safety.

Common challenges
Recommended systems
PLC-controlled industrial RO with 4040/8040 membranes removing 95–99.5% of dissolved salts.
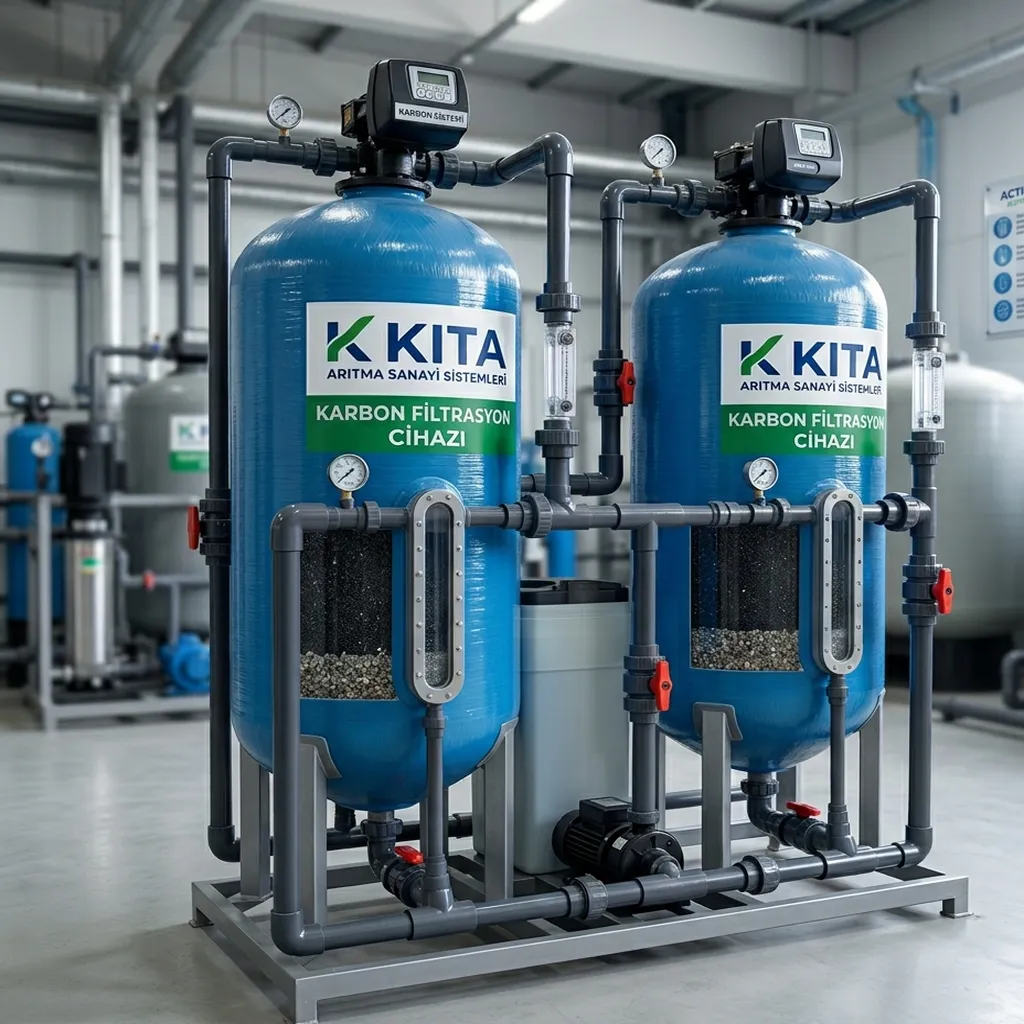
Removes chlorine, odour, colour and organics; protects RO membranes from chlorine.
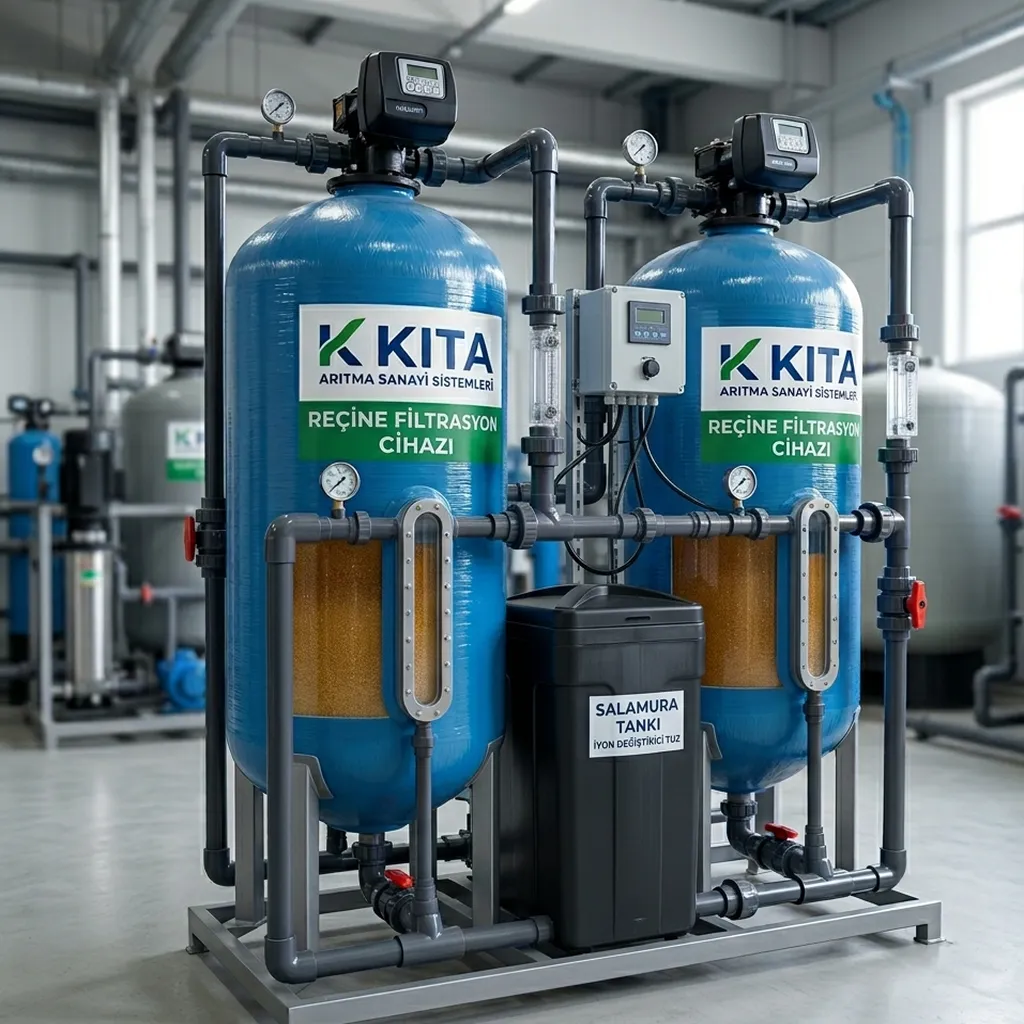
Automatic softeners that prevent scale and save energy.
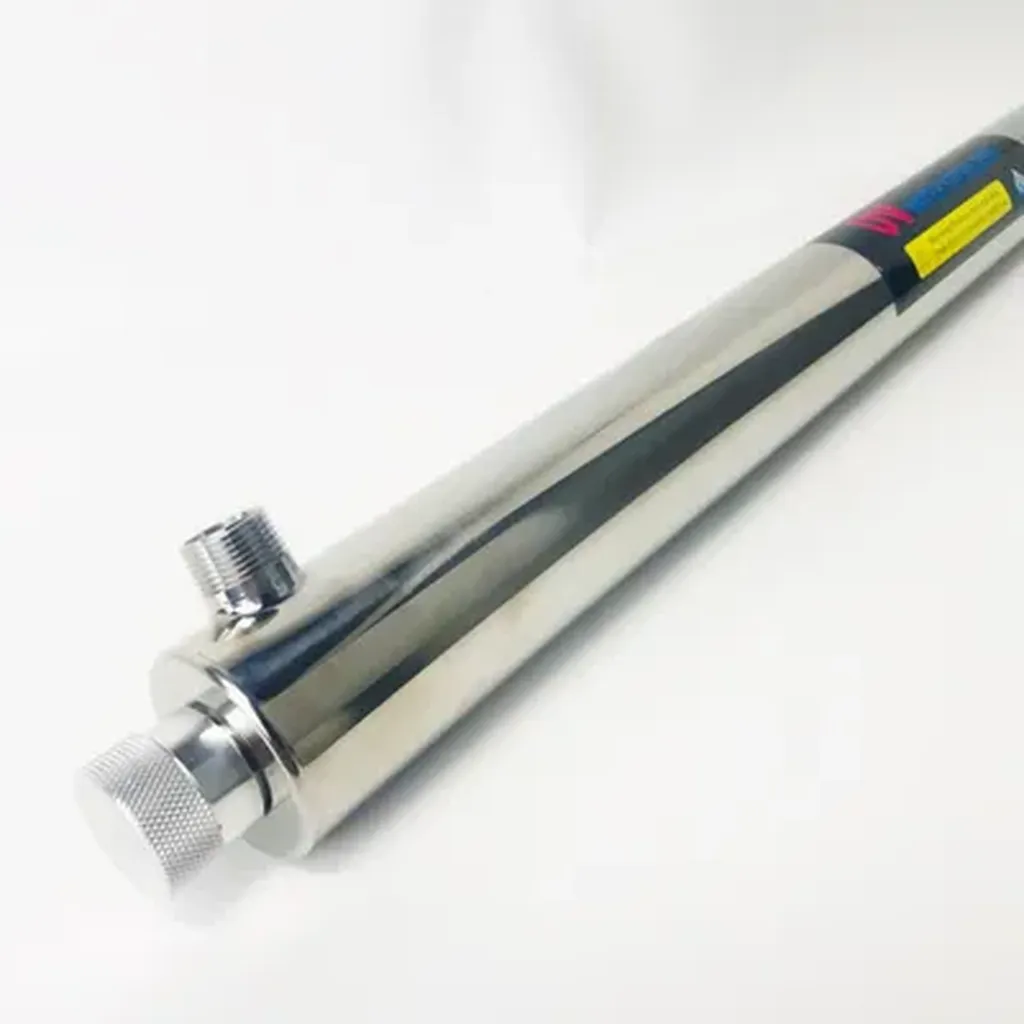
Chemical-free disinfection: stainless UV sterilisers, original lamps and quartz sleeves.
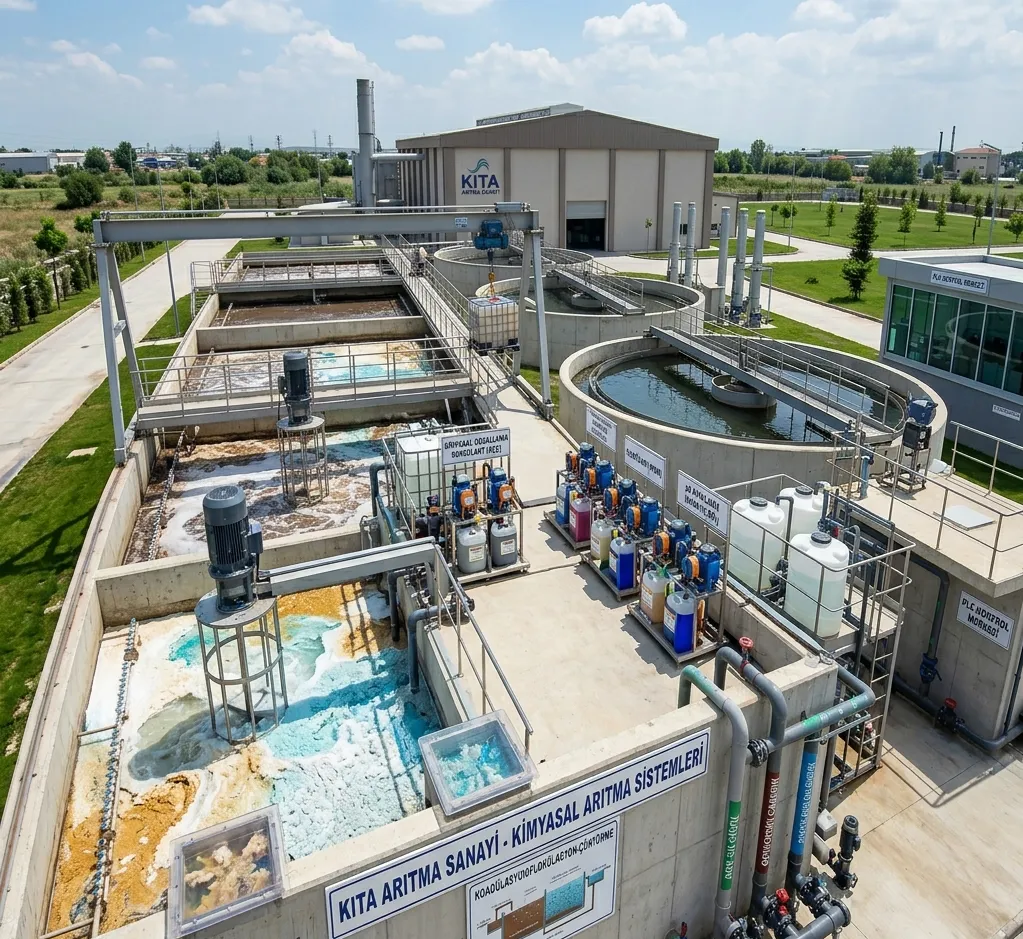
Neutralisation-coagulation-flocculation plants for plating, textile, automotive and chemical effluent.
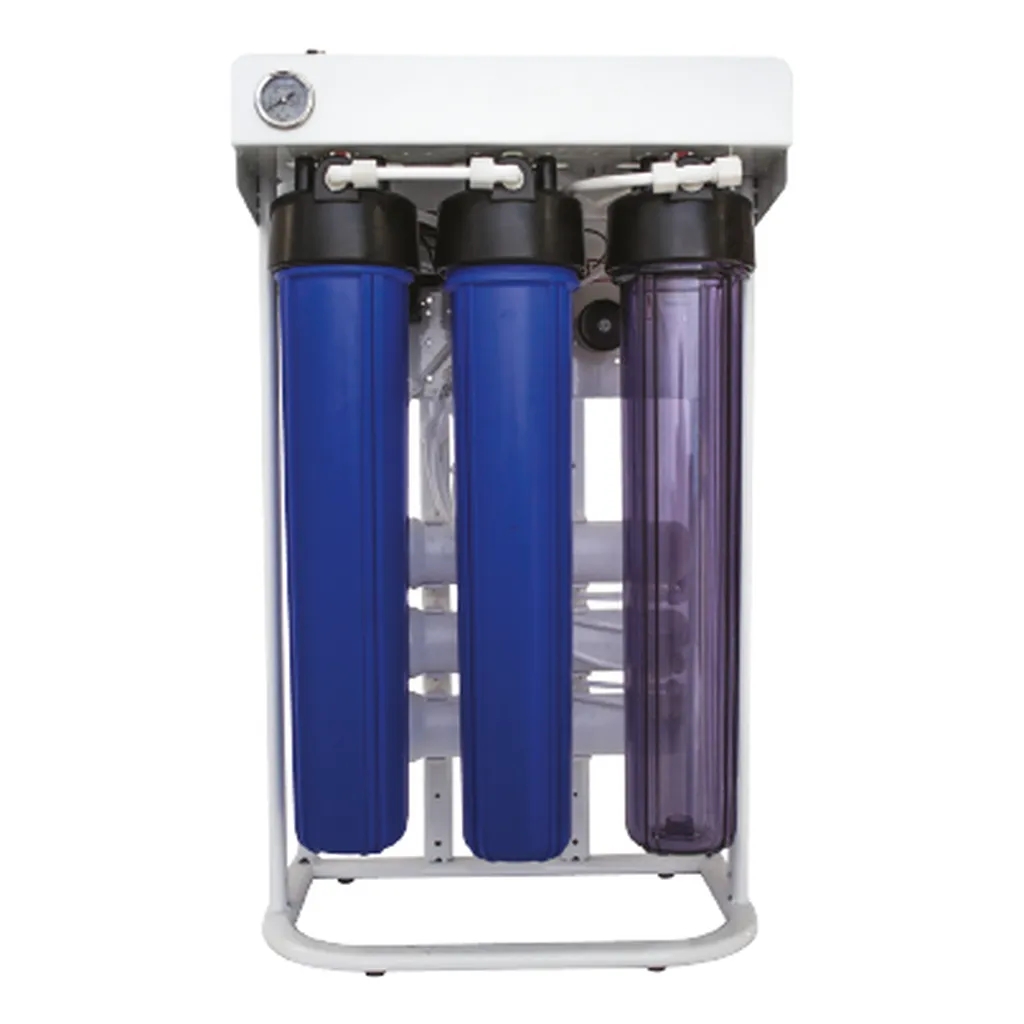
High-flow systems for kitchens and cafés that protect coffee, tea and ice machines.
In food and beverage production water is an ingredient. Reverse osmosis delivers consistent process water regardless of seasonal changes; carbon removes chlorine taste; softening protects boilers and pasteurisers; UV adds a microbiological barrier; and chemical treatment brings effluent within limits.
We will quickly send the right solution and price based on your capacity and water analysis.
Get a Quote WhatsApp 0533 590 30 82 Mon–Sat 08:30–18:30 · Sun Emergency serviceFree site survey & water analysis
We survey your site and analyse your raw water, then present the system that fits your needs and budget in a technical report.